Skip to content
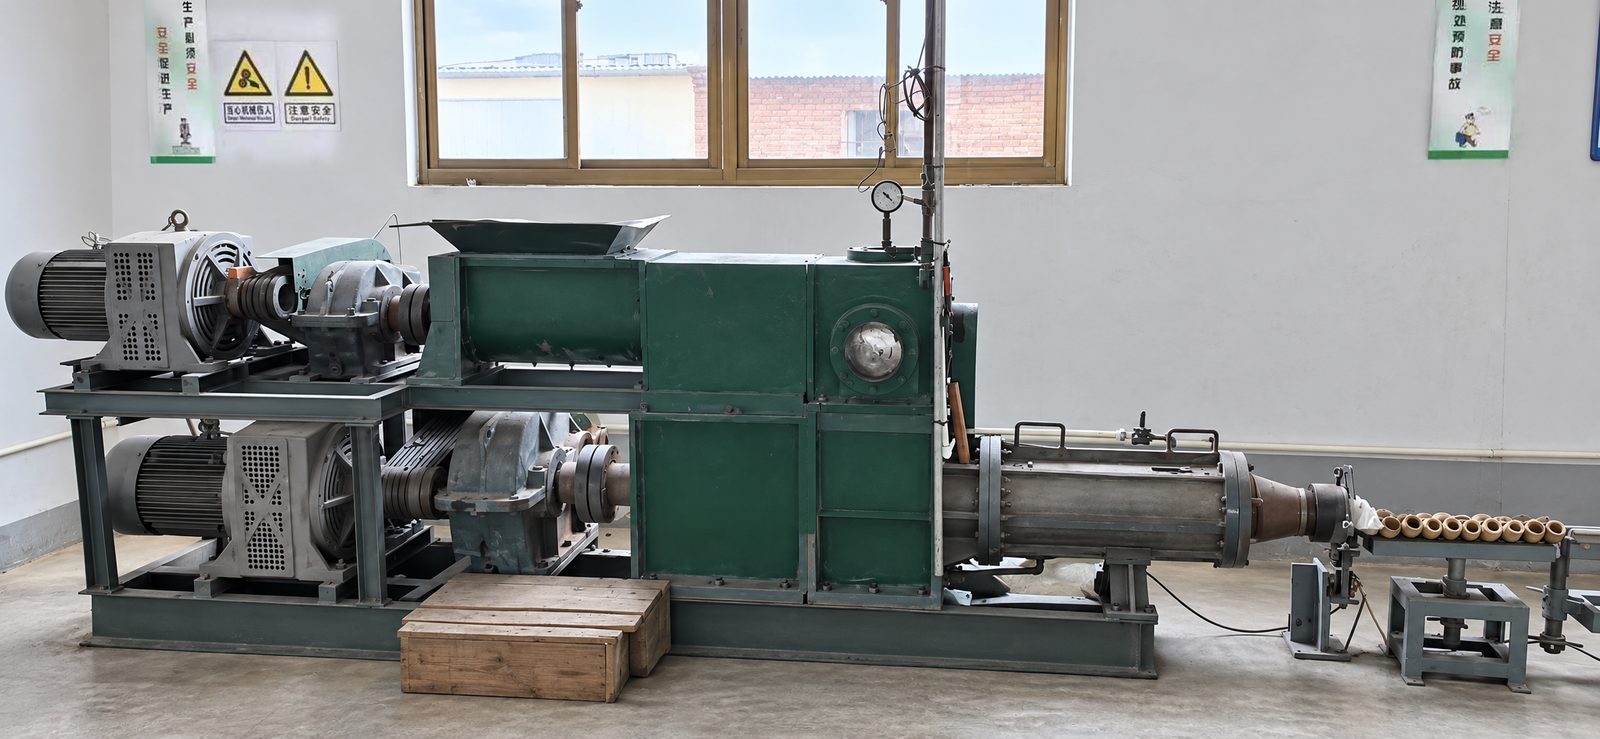
A dark-green two-stage horizontal extruder along a white workshop wall, with a feed hopper on top and the extrusion barrel ending at a support rail on the right.

Our factory

An industrial ceramics manufacturer in Tangshan, Hebei.

GY Alumina manufactures alumina thermocouple protection tubes, insulators, furnace tubes, crucibles and custom ceramic parts at our factory in Tangshan, Hebei, China. Our Chinese trademark is 鑫国玉™, Xin Guo Yu.

鑫国玉™ XIN GUO YU logo
Legal name
唐山市高铝刚玉工业陶瓷厂
Name on ISO certificate
Tangshan High Aluminum Corundum Industrial Ceramics Factory

Where we are

Tangshan, Hebei

Our factory is in Xiaoji Town, Fengnan District, Tangshan, Hebei, China.

Our industrial ceramics serve thermocouple makers, furnace builders, laboratories and equipment manufacturers.

Standard sizes are usually in stock and cut to the ordered length. Small standard orders usually ship in about 3 days; bulk orders in about 7 days. Parts made to drawing usually take 25–30 days, with a usual minimum of 100 pieces. Compare product sizes and configurations or send a drawing for a quotation.

Town
Xiaoji Town
District
Fengnan District
City
Tangshan
Province
Hebei

Track record

customers served
100+
repeat customers
100+
pieces shipped, 2024⁠–⁠2026
1.4 million+
alumina tubes shipped since 1984
21 million

We supplied thermocouple protection tubes for the expansion of China’s solar industry.

Pieces shipped 2024⁠–⁠2026: from our sales records.

Capabilities

Four forming routes, and parts made to your drawing.

Forming methods

  • Slip casting
  • Pressing
  • Extrusion
  • Hot pressing

Services

  • Design from customer drawings or samples
  • Custom industrial ceramic fabrication
  • Special-shaped ceramic parts
  • Pressed and extruded oxide components
  • Product research and development

Industries our products serve

  • Temperature sensing and instrumentation
  • Industrial furnaces and heat treatment
  • Steel and metallurgy
  • Electronics
  • Electrical insulation
  • Chemical processing
  • Glass
  • Laboratory equipment and analysis
  • Scientific research
  • Machinery and industrial equipment
  • Textiles

How we make it

From alumina powder to a packed crate, in one factory.

Milling, forming, firing, finishing and packing all happen in our own factory. Send your drawing and we confirm the route, grade and tolerances at quotation.

  1. 01

    Raw material

    We start from calcined alumina powder.

  2. 02

    Milling

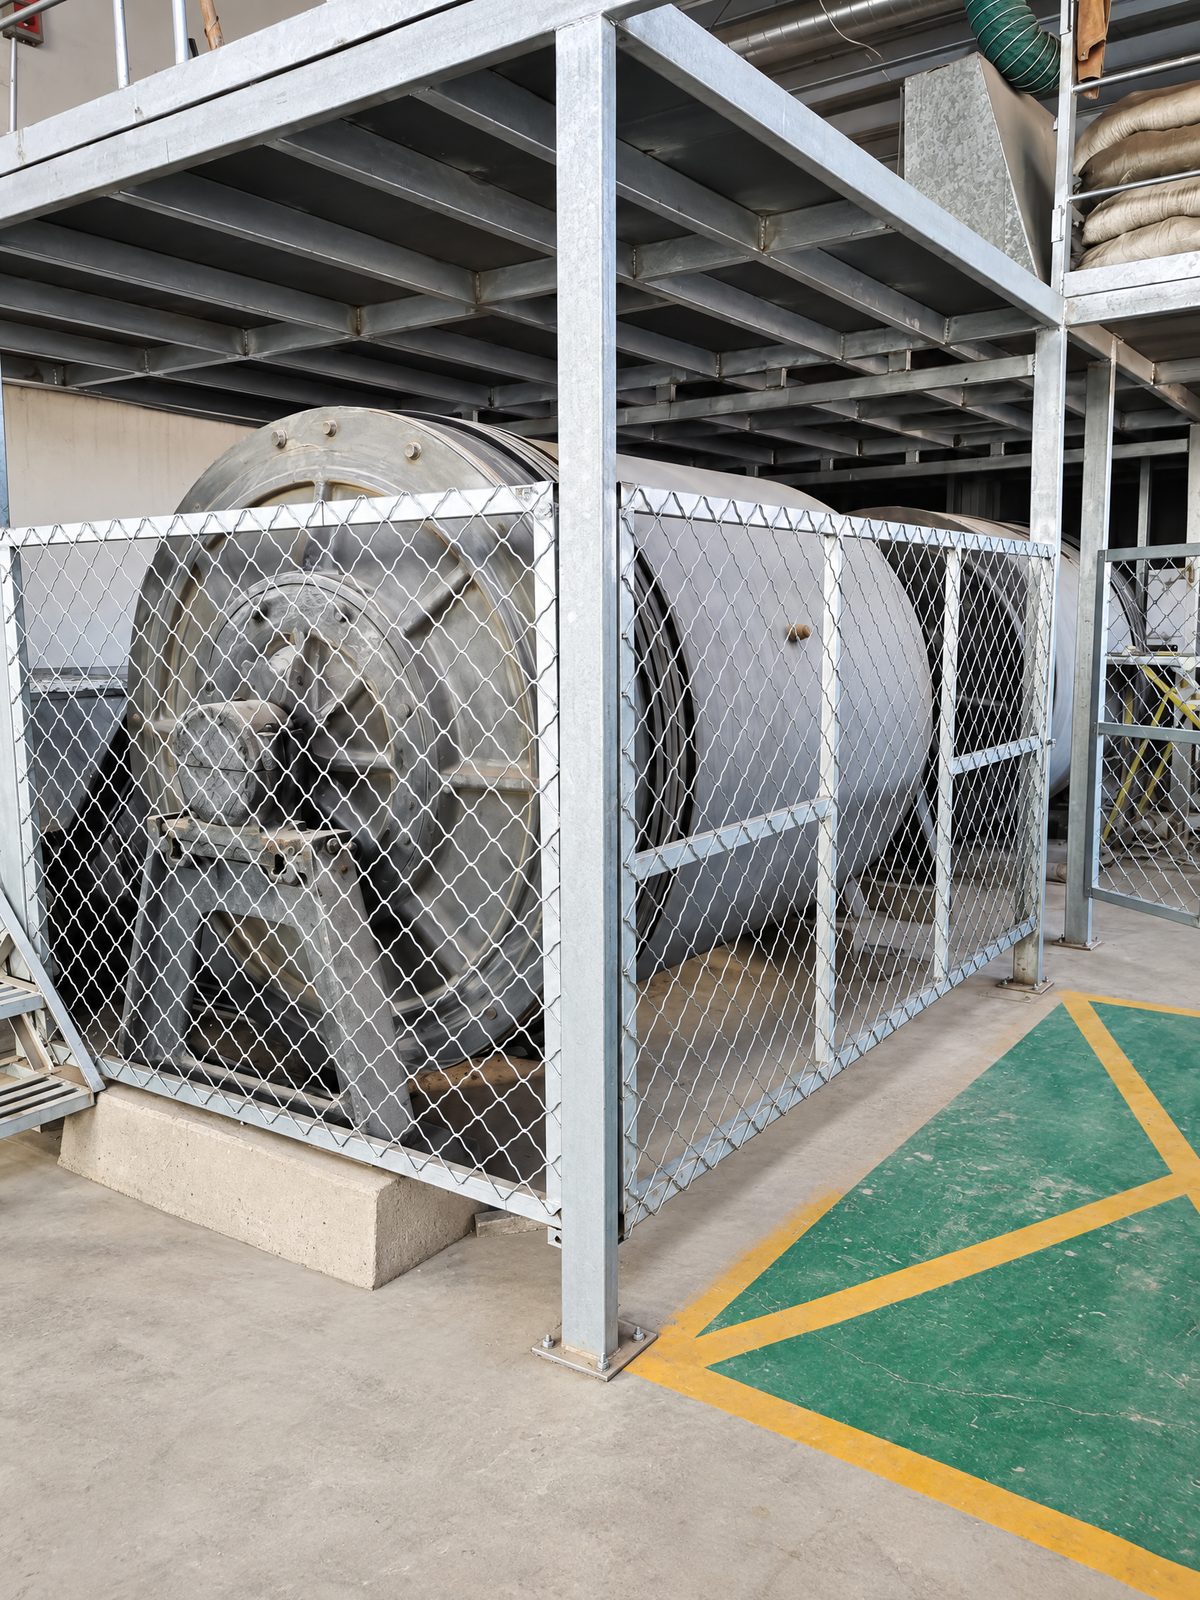
    The powder is milled in large drum ball mills.

    Two large grey drum ball mills inside a galvanised steel frame with diamond-mesh safety panels, under a steel mezzanine.
    Drum ball mills behind safety mesh.
  3. 03

    Forming

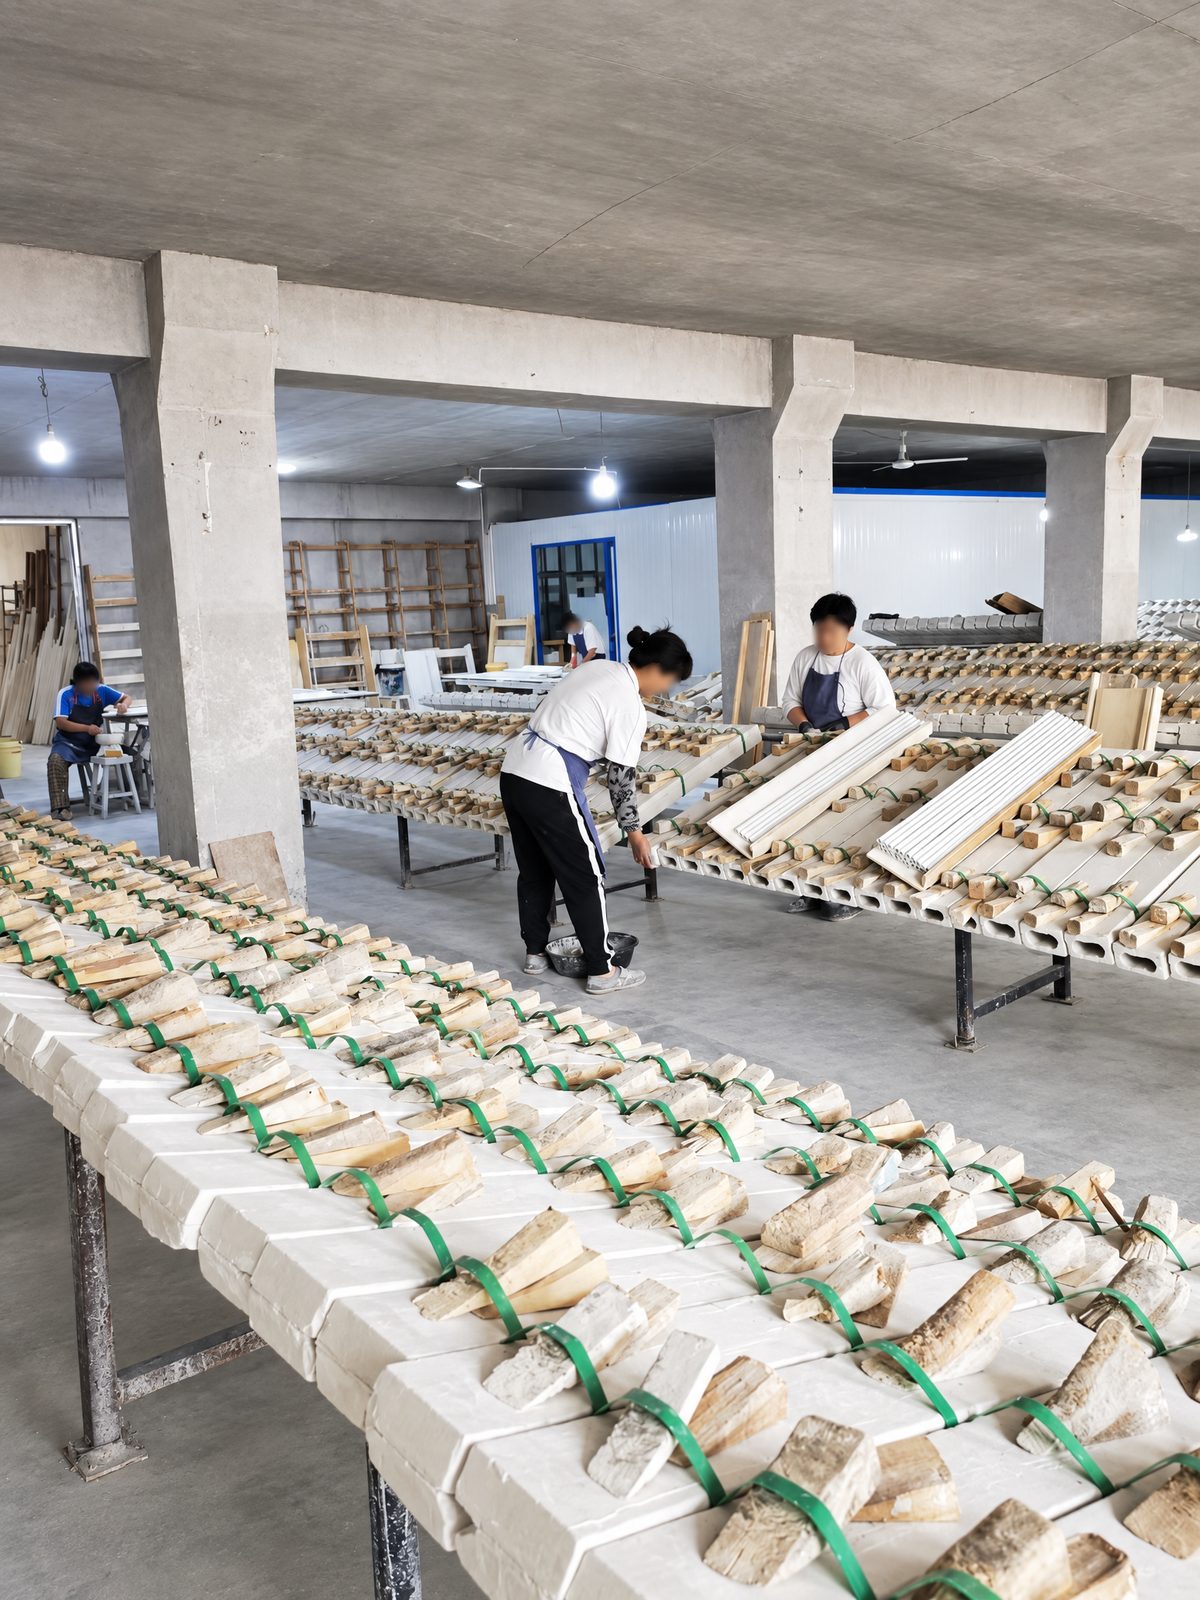
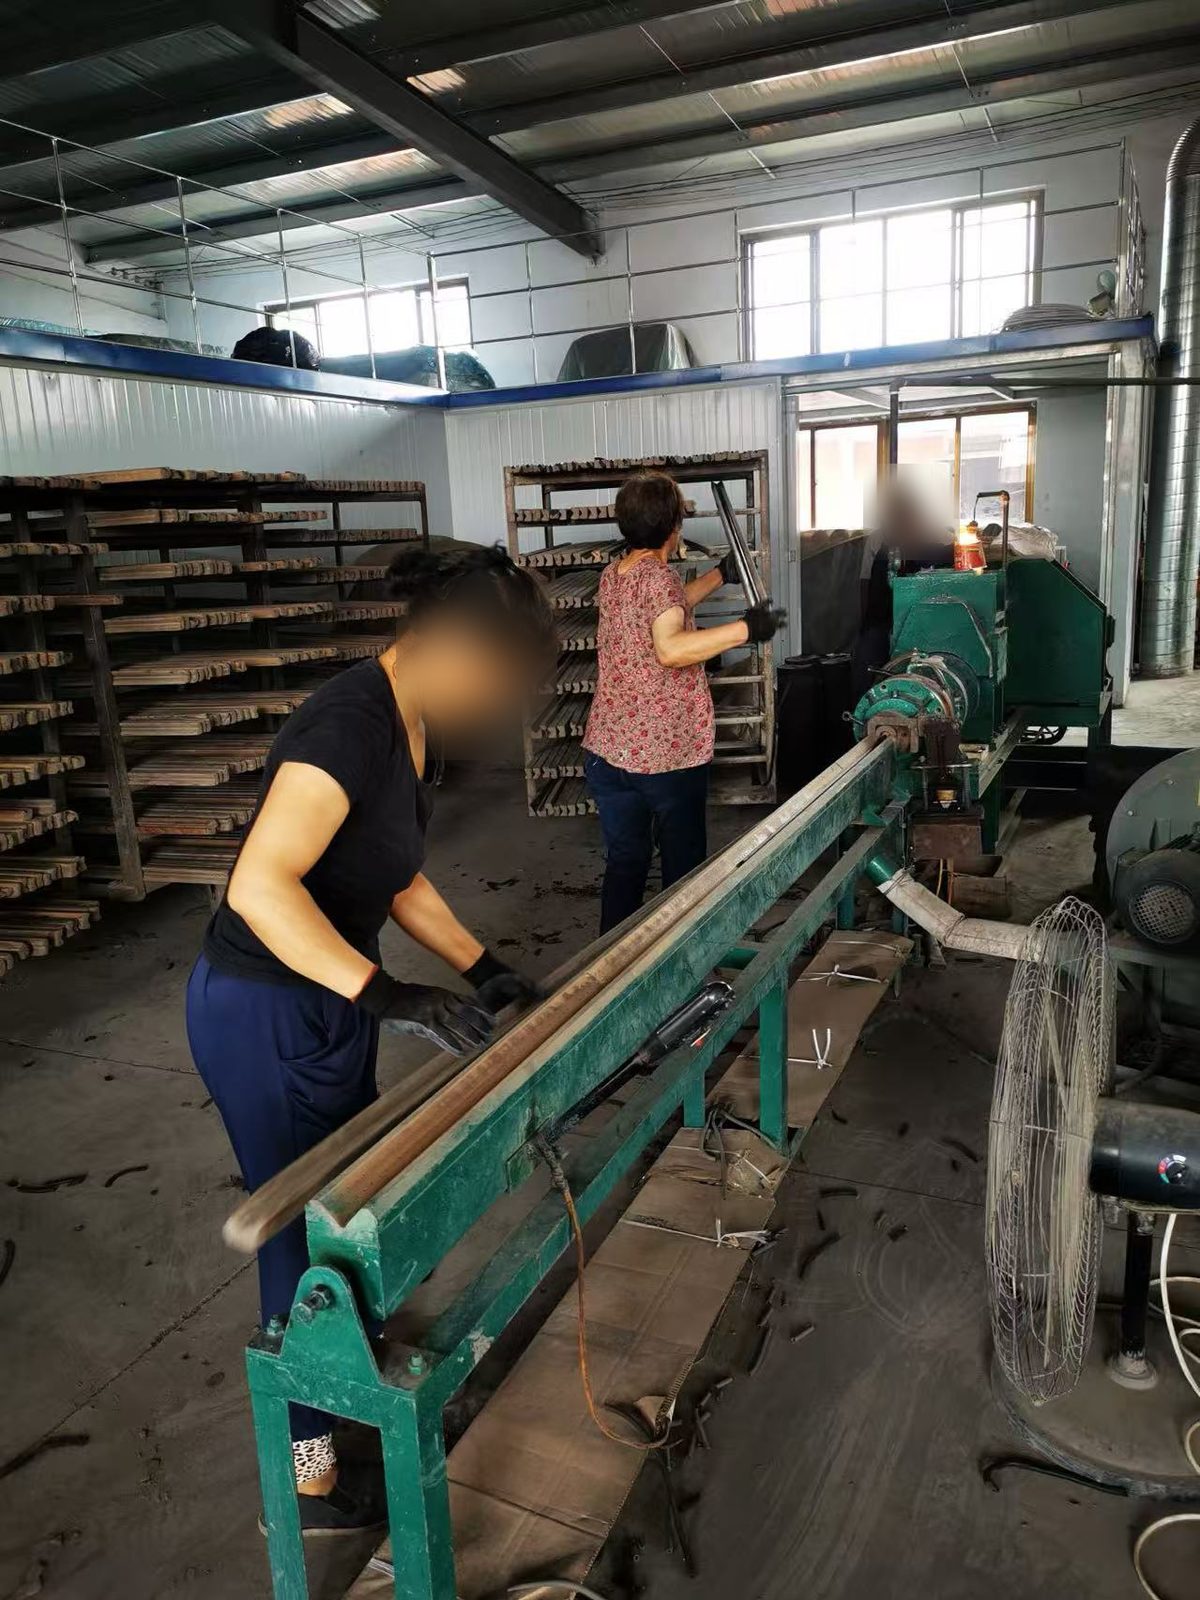
    Tubes and rods are formed on horizontal vacuum extruders and a vertical hydraulic ram extruder; slip casting uses plaster moulds.

    A dark-green two-stage horizontal extruder along a white workshop wall, with a feed hopper on top and the extrusion barrel ending at a support rail on the right.
    Two-stage horizontal vacuum extruder.
  4. 04

    Drying

    Formed pieces dry on multi-tier rack carts and grooved boards before firing.

  5. 05

    Firing

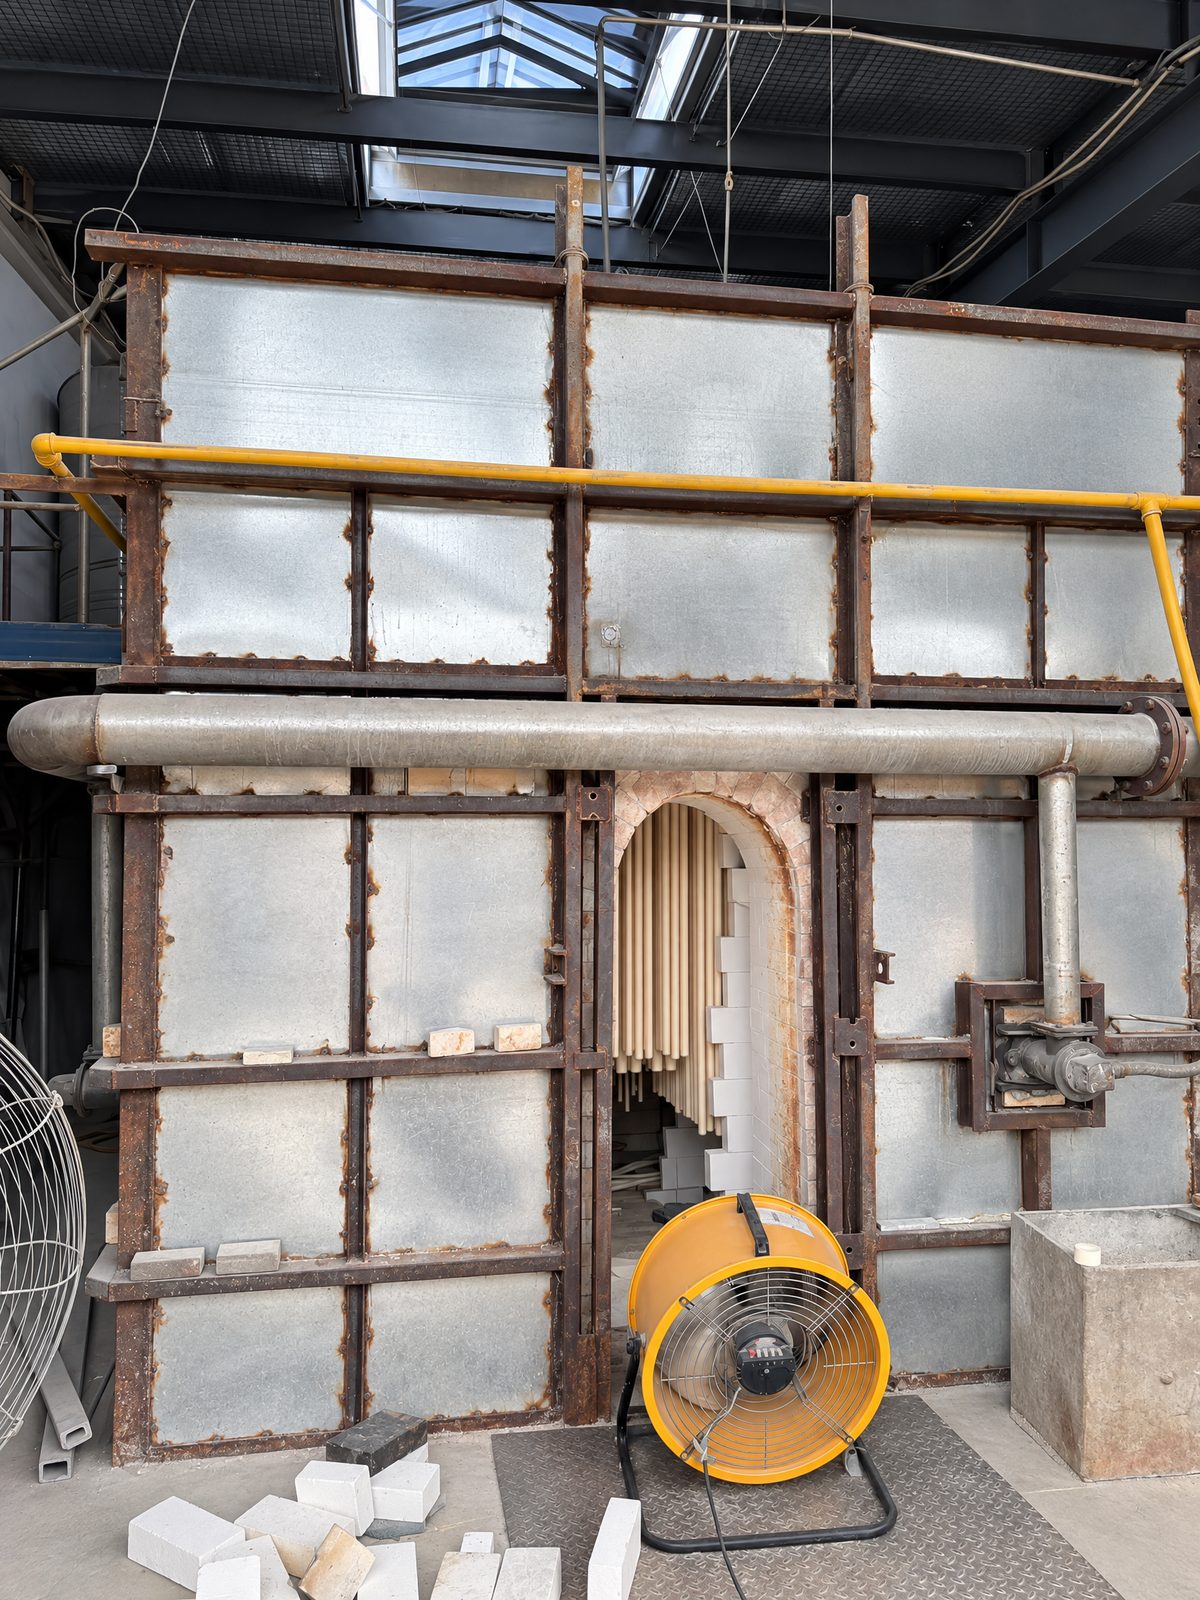
    Tubes hang vertically in the kiln, and our written gas-kiln procedure controls firing with thermocouples and an optical pyrometer.

    A large gas-fired kiln with a steel-framed front; through the arched door, long ceramic tubes hang inside.
    Long tubes hung inside a gas-fired kiln.
  6. 06

    Finishing

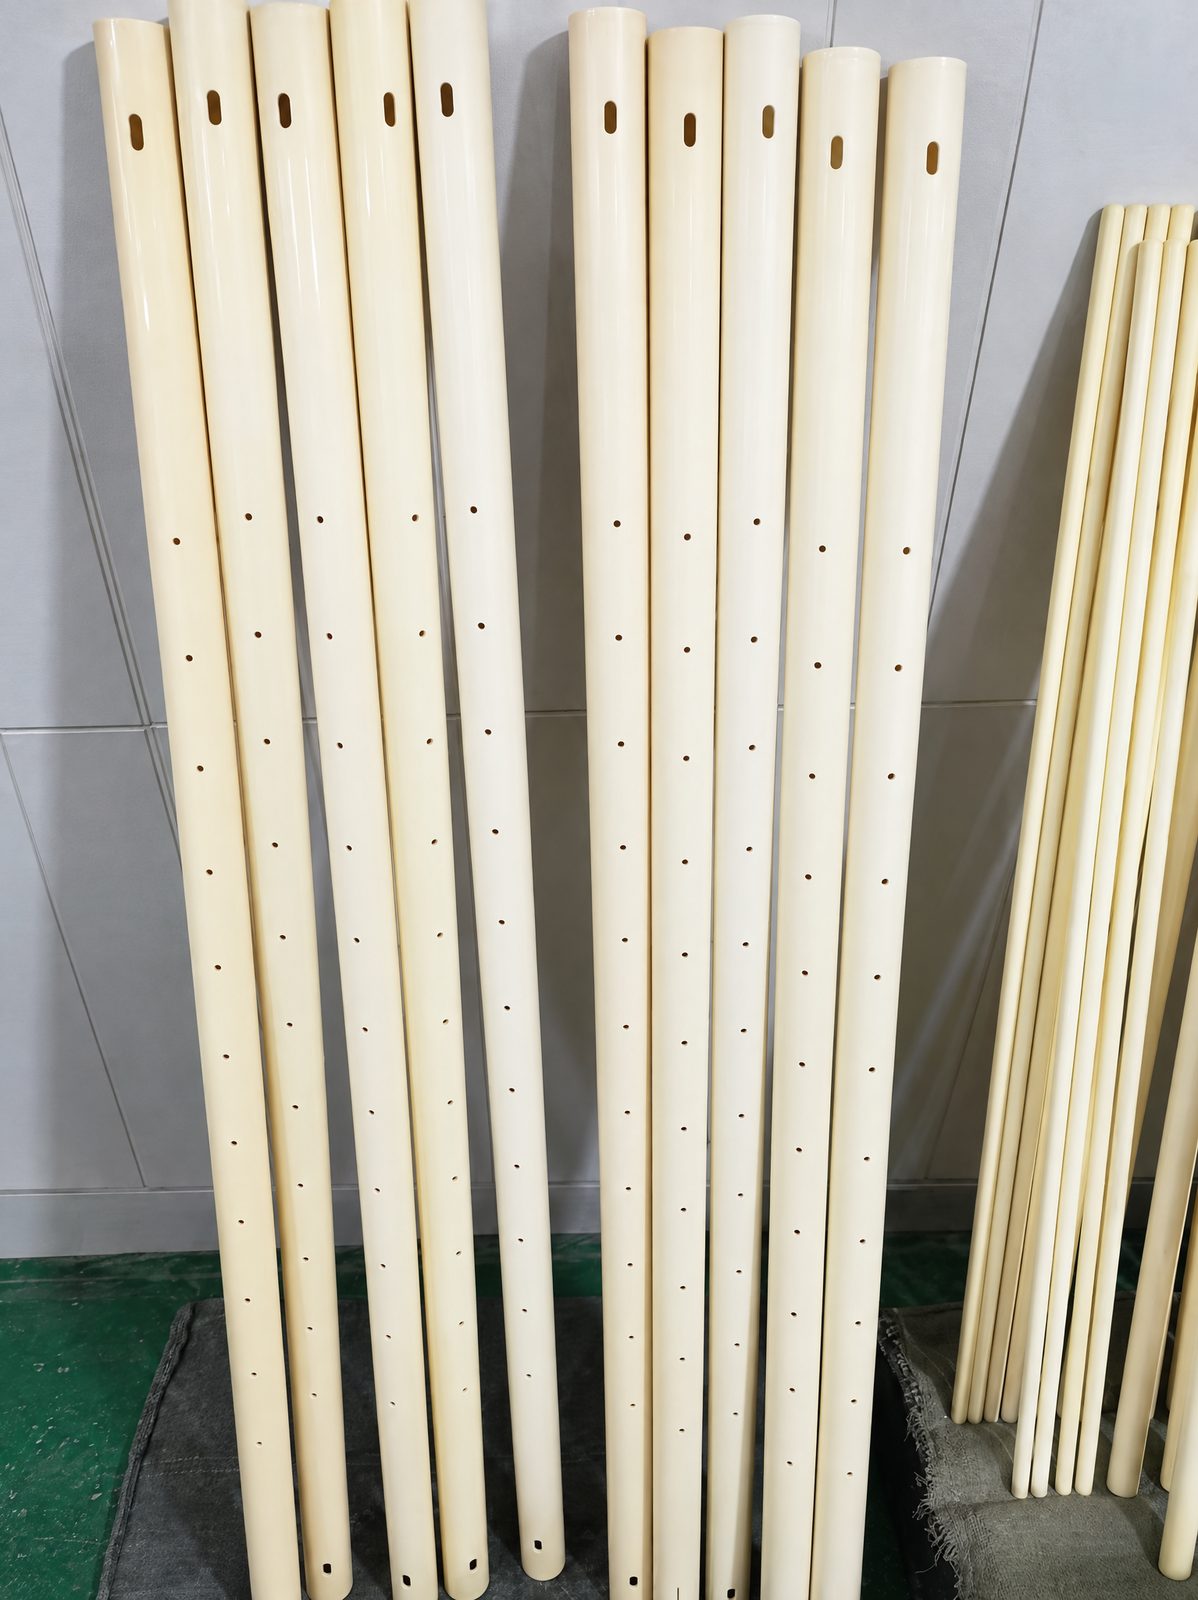
    Tubes are cut to the ordered length, then slotted or drilled where the drawing calls for it.

    Ivory ceramic tubes standing against a plain grey background, each with an oblong slot near the top and a line of small round holes down one side.
    Tubes with a cut slot and a line of side holes.
  7. 07

    Inspection

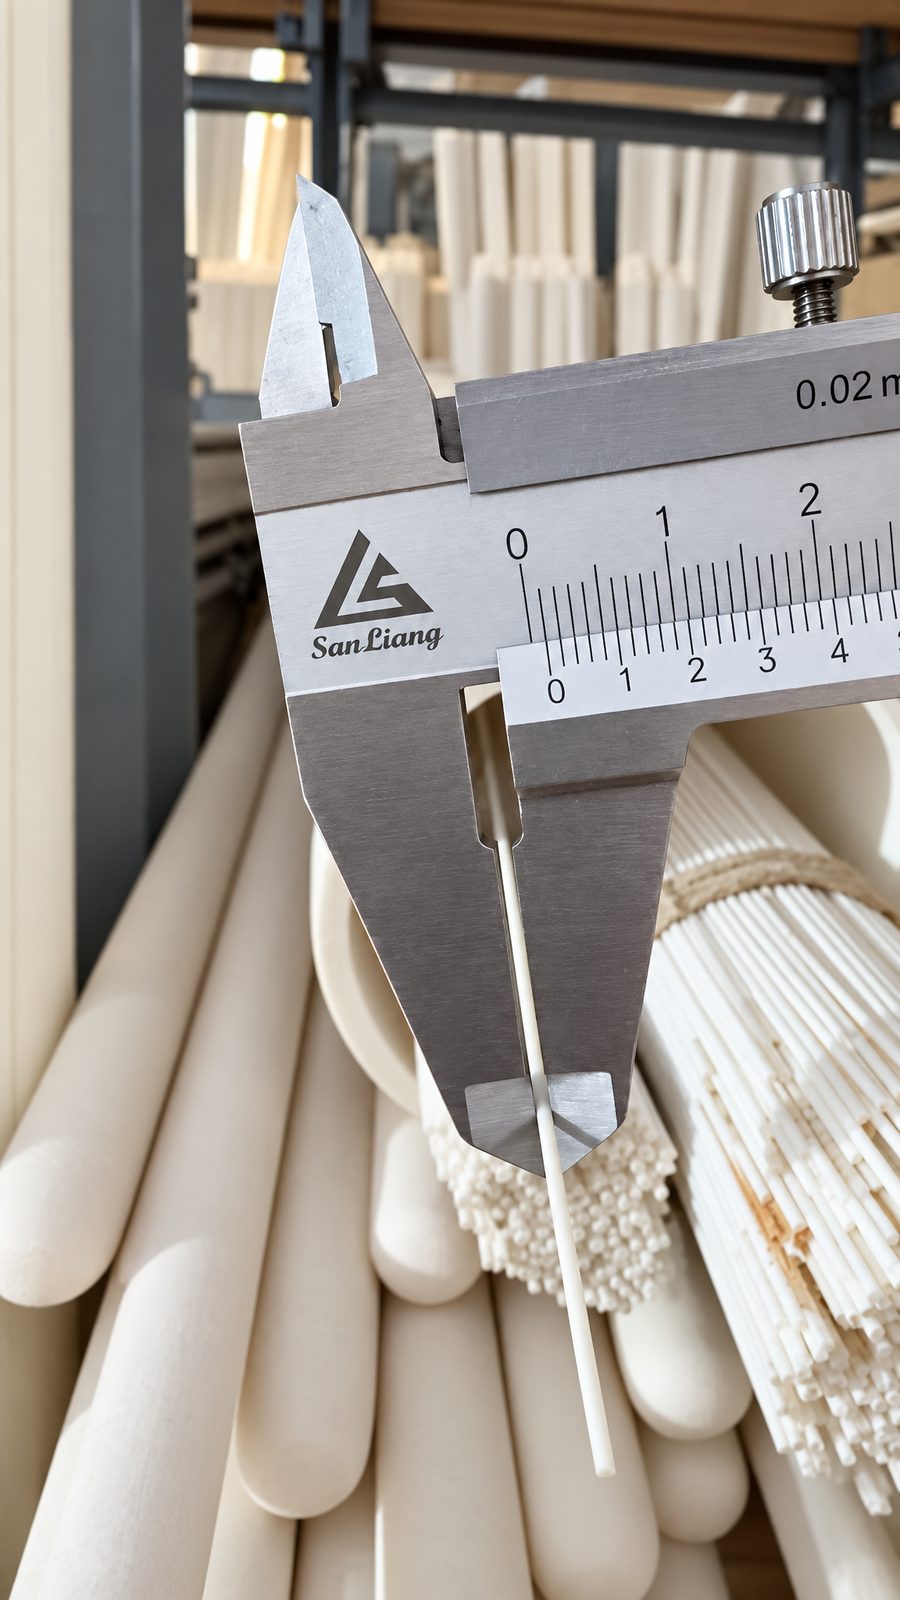
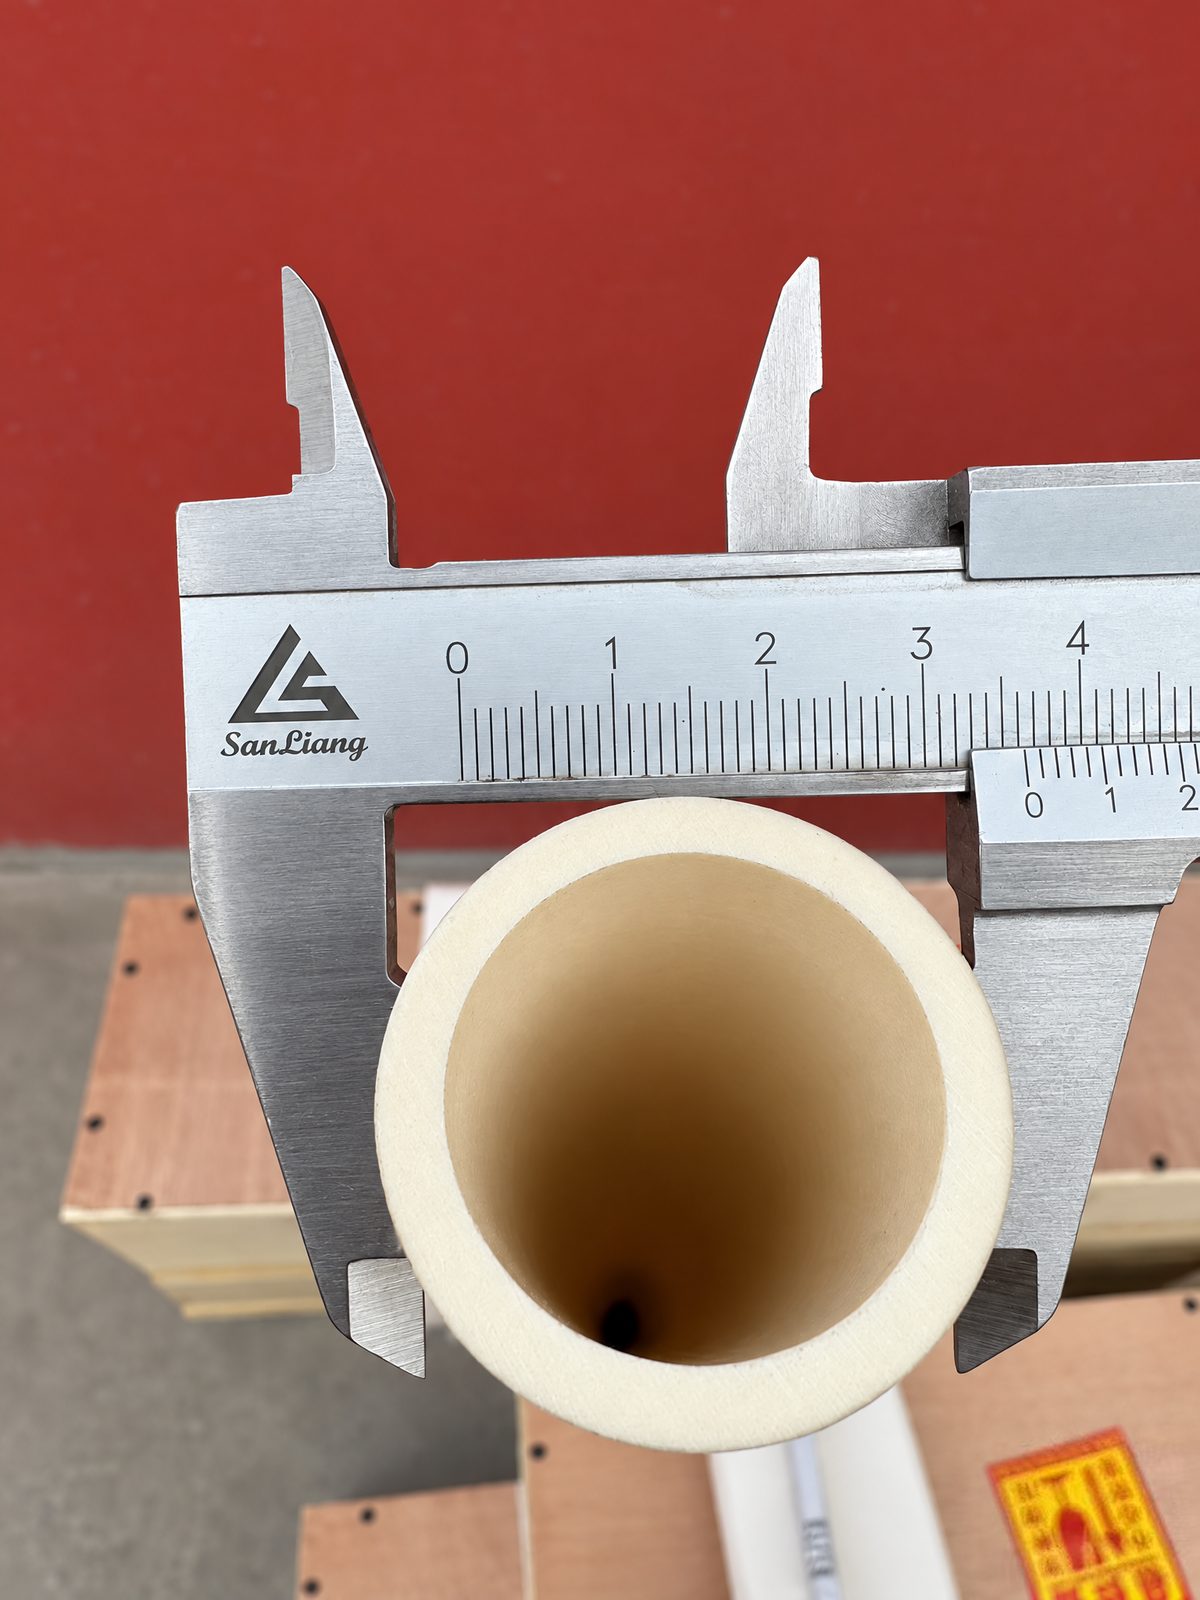
    Outside and inside diameters are measured with vernier calipers.

    A steel vernier caliper with its jaws across the outside diameter of a thick-walled cream ceramic tube, seen end-on.
    Measuring the outside diameter of a large tube.
  8. 08

    Packing

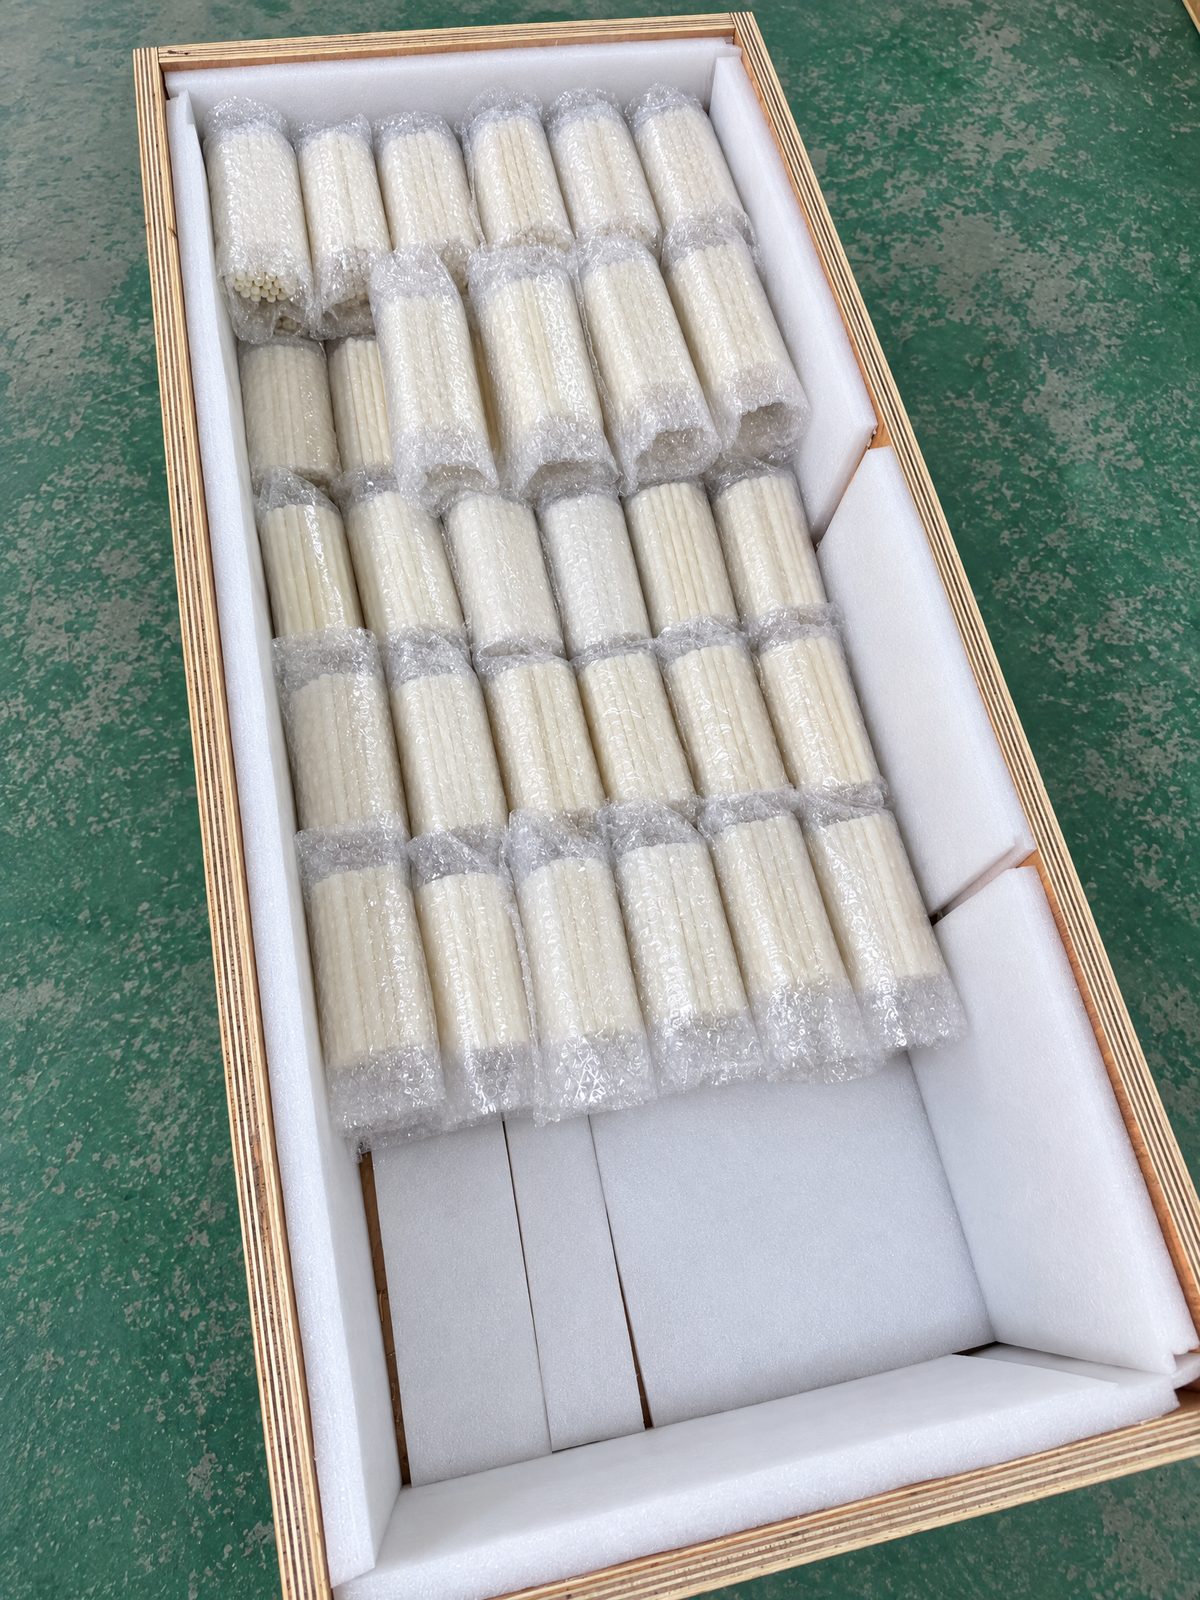
    Tubes are bubble-wrapped or bundled and packed in foam-lined plywood crates.

    An open plywood crate lined with white foam on all sides, holding rows of bubble-wrapped bundles of short ivory tubes.
    Bubble-wrapped bundles in a foam-lined crate.

Continuity

The same product line for 15+ years.

Every product, material and capability we list is in production today. The factory has been running for 42 years, and we have made this product line for at least 15 years. Buyers who qualify a part with us keep ordering it: 100+ of our customers come back to us with repeat orders.

years in operation
42
repeat customers
100+

Certified and tested

Certified to ISO 9001:2015, with independent lab results.

Quality management

ISO 9001:2015

GB/T19001-2016 · certified by CFL Certification Center

Scope
Manufacturing of ceramic protective tubes for thermocouples
Registration
06525Q02034R1S
Valid
6 August 2025 – 5 August 2028
Accreditation
CNAS C065-M · IAF

The issuer listed this certificate as valid when checked on 6 October 2026. Check the issuer’s record (Chinese).

A copy of the certificate is available on request.
Independent lab test

99.61% Al₂O₃

Alumina tube sample, tested by Chinalco Testing Technology (Zhengzhou) Co., Ltd., 13 May 2026. Report 26-04928.

Chemical composition of the tested alumina tube sample
Item%Method
Al₂O₃99.61GB/T 24487-2022
SiO₂0.15GB/T 6609.3-2004
Fe₂O₃0.014GB/T 6609.4-2004
Na₂O0.054GB/T 6609.1-2018
CaO0.13GB/T 6609.1-2018
Loss on ignition0.033GB/T 6609.2-2022

Tested by the same lab every year

  • 202499.55% Al₂O₃, report 24-04372
  • 202599.57% Al₂O₃, report 25-04979
  • 202699.61% Al₂O₃, report 26-04928

Lab reports are available on request.

See the certificate and the lab report

Photographs

Inside the factory

Forming

Two workers at a green horizontal extrusion machine on the forming line.
The extrusion line.
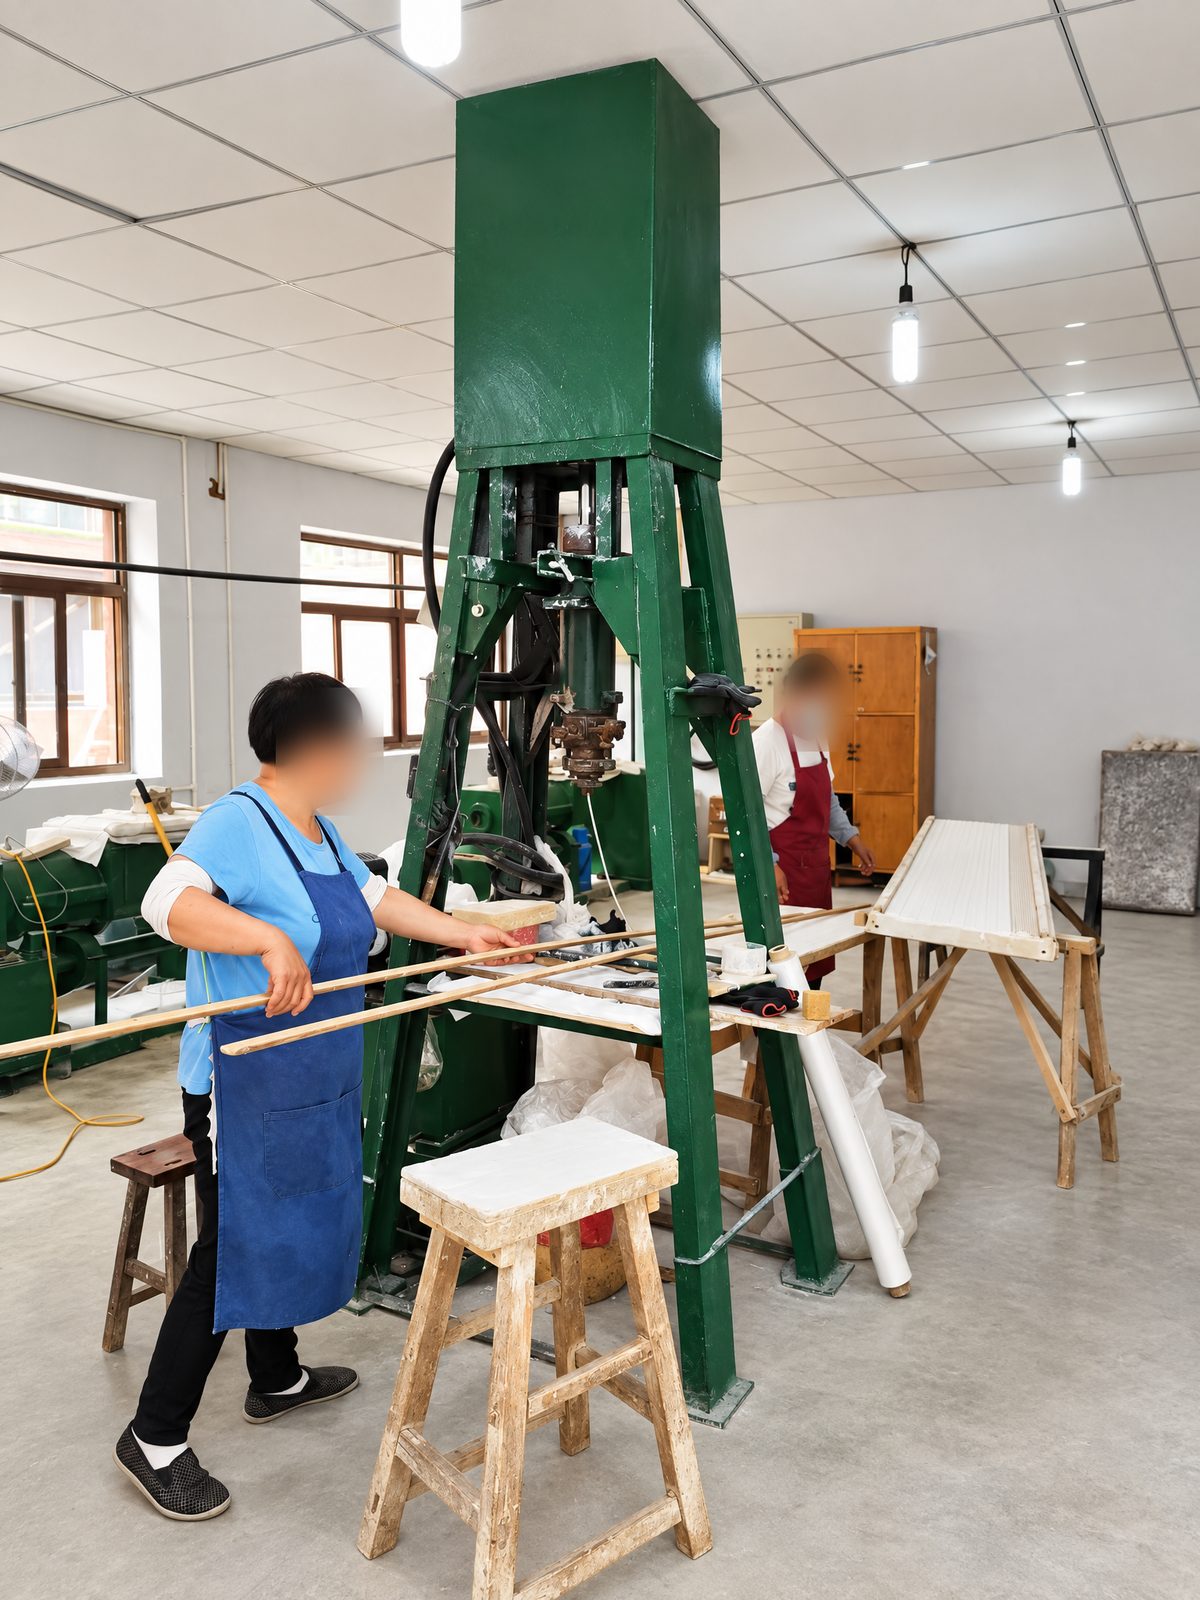
An operator beside a tall green vertical hydraulic press used to form ceramic parts.
Hydraulic forming press.
Long tables of strapped casting moulds laid out across the forming hall.
Casting moulds laid out in the forming hall.
A steel vernier caliper measuring the outside diameter of a ceramic tube during inspection.
Checking a tube diameter with calipers.

Finished stock and packing

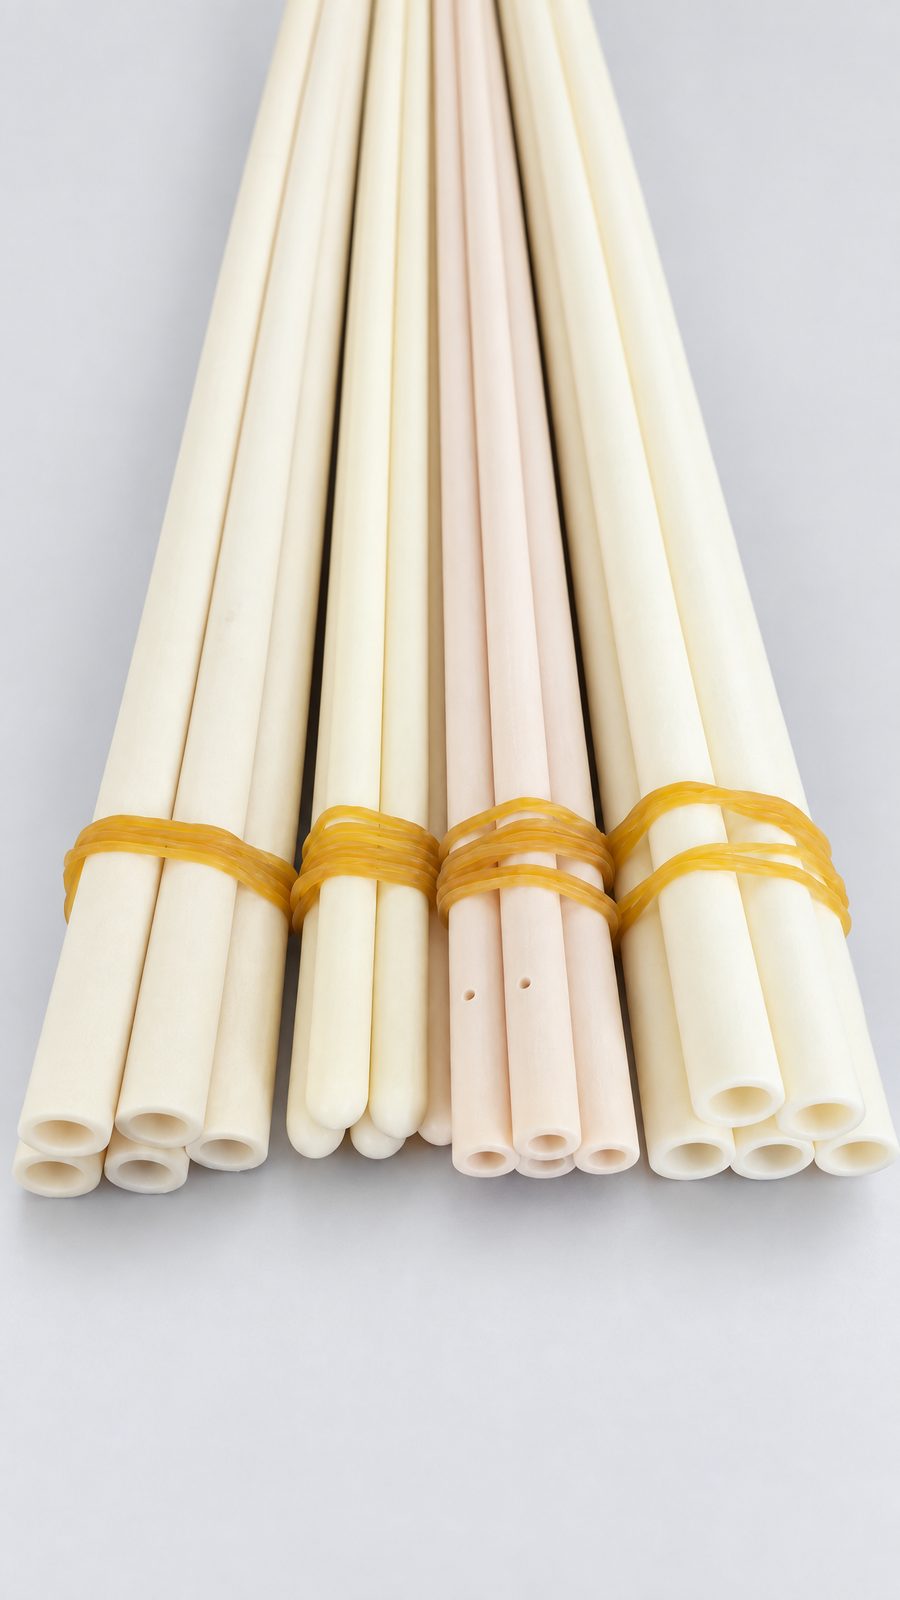
Bundles of long cream-coloured alumina protection tubes with closed ends, tied with yellow bands, on a dark charcoal-grey background.
Closed-end protection tubes.
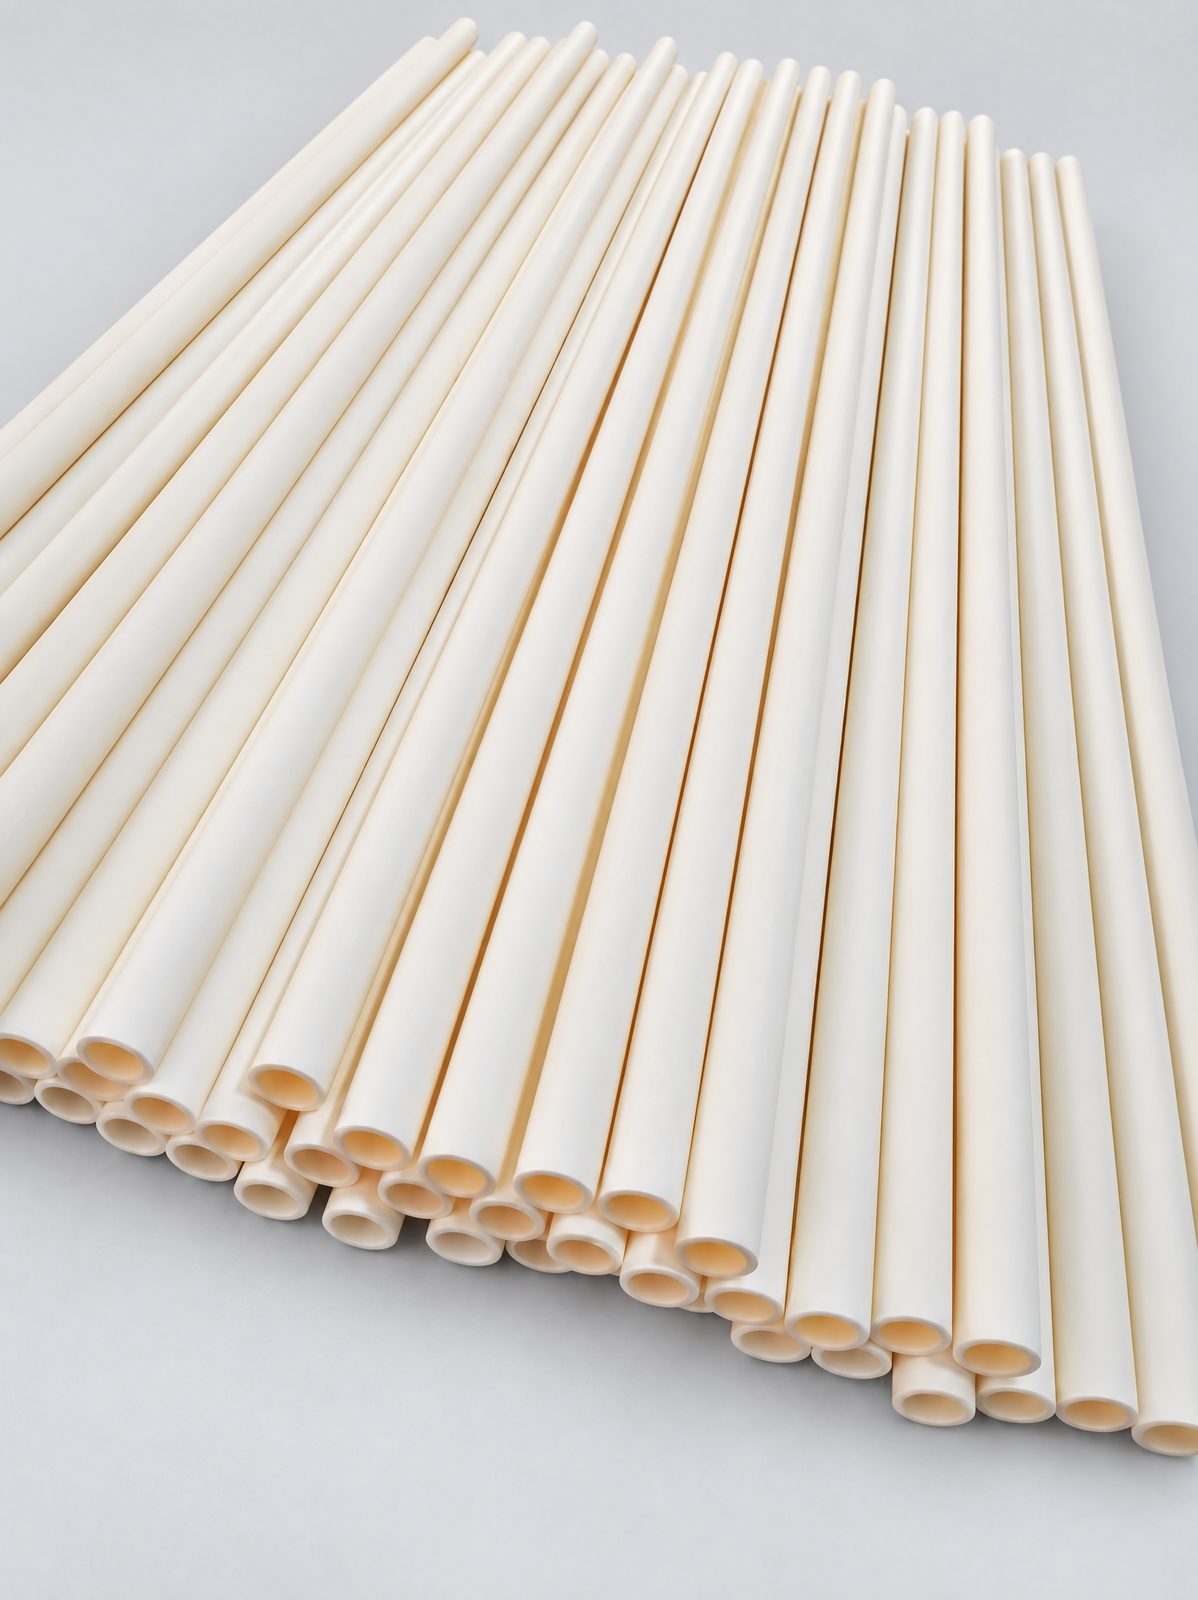
A long row of finished alumina tubes laid side by side on a dark charcoal-grey background.
Finished tubes before packing.
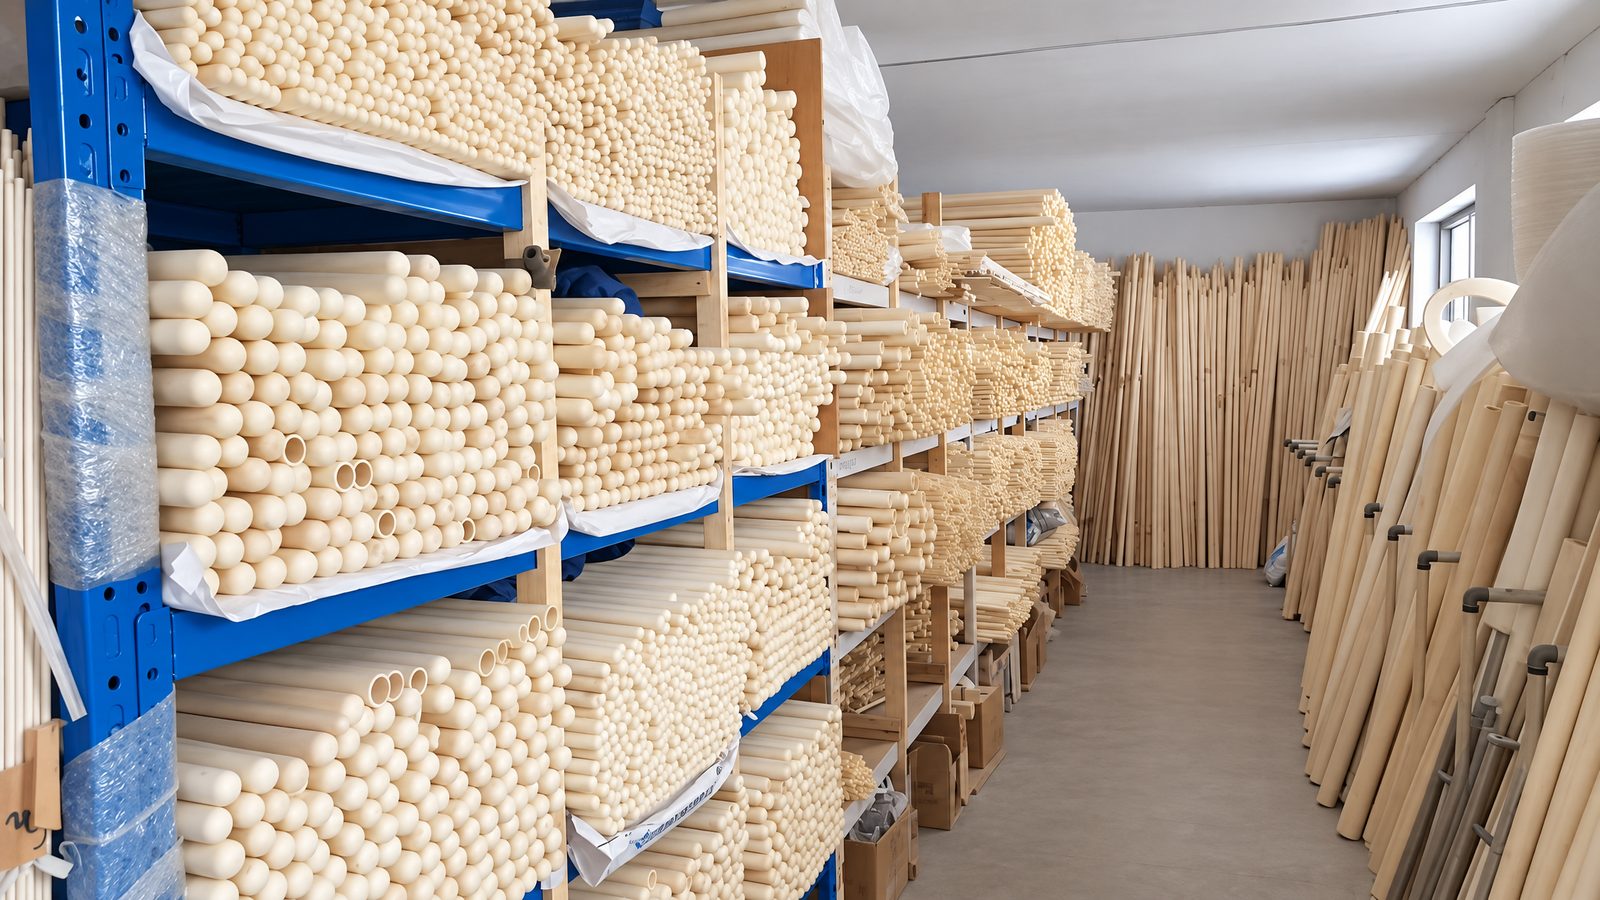
Factory storeroom with blue metal shelving stacked with finished ceramic tubes and parts.
Finished stock in the storeroom.
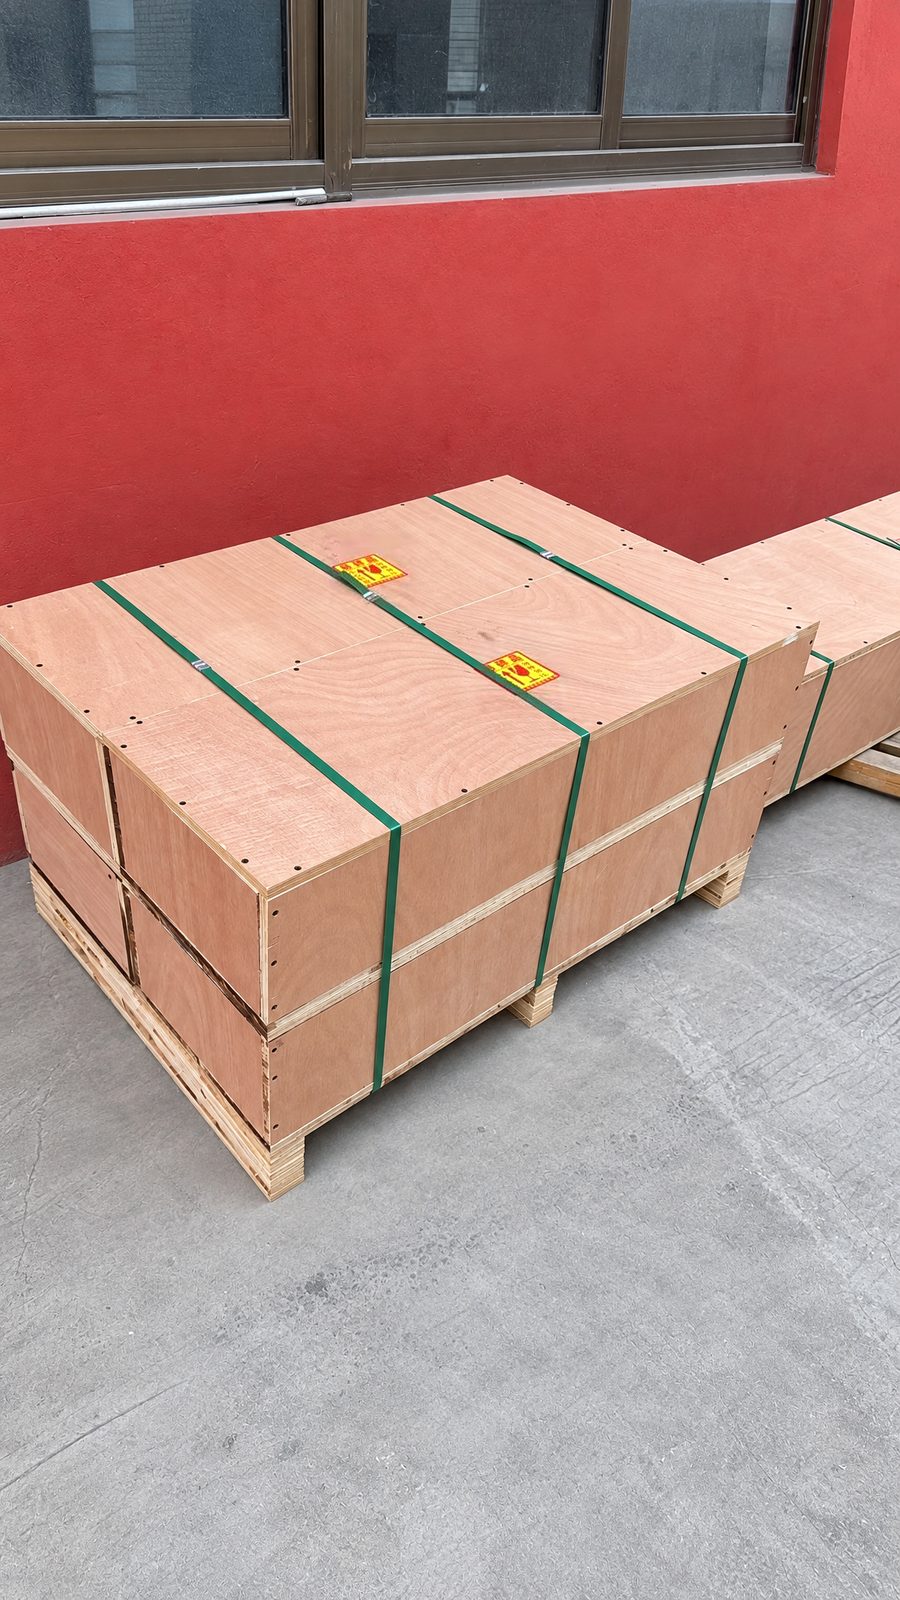
Wooden export crates, strapped and stacked on a pallet, ready for shipment.
Wooden export crates on a pallet.

Firing

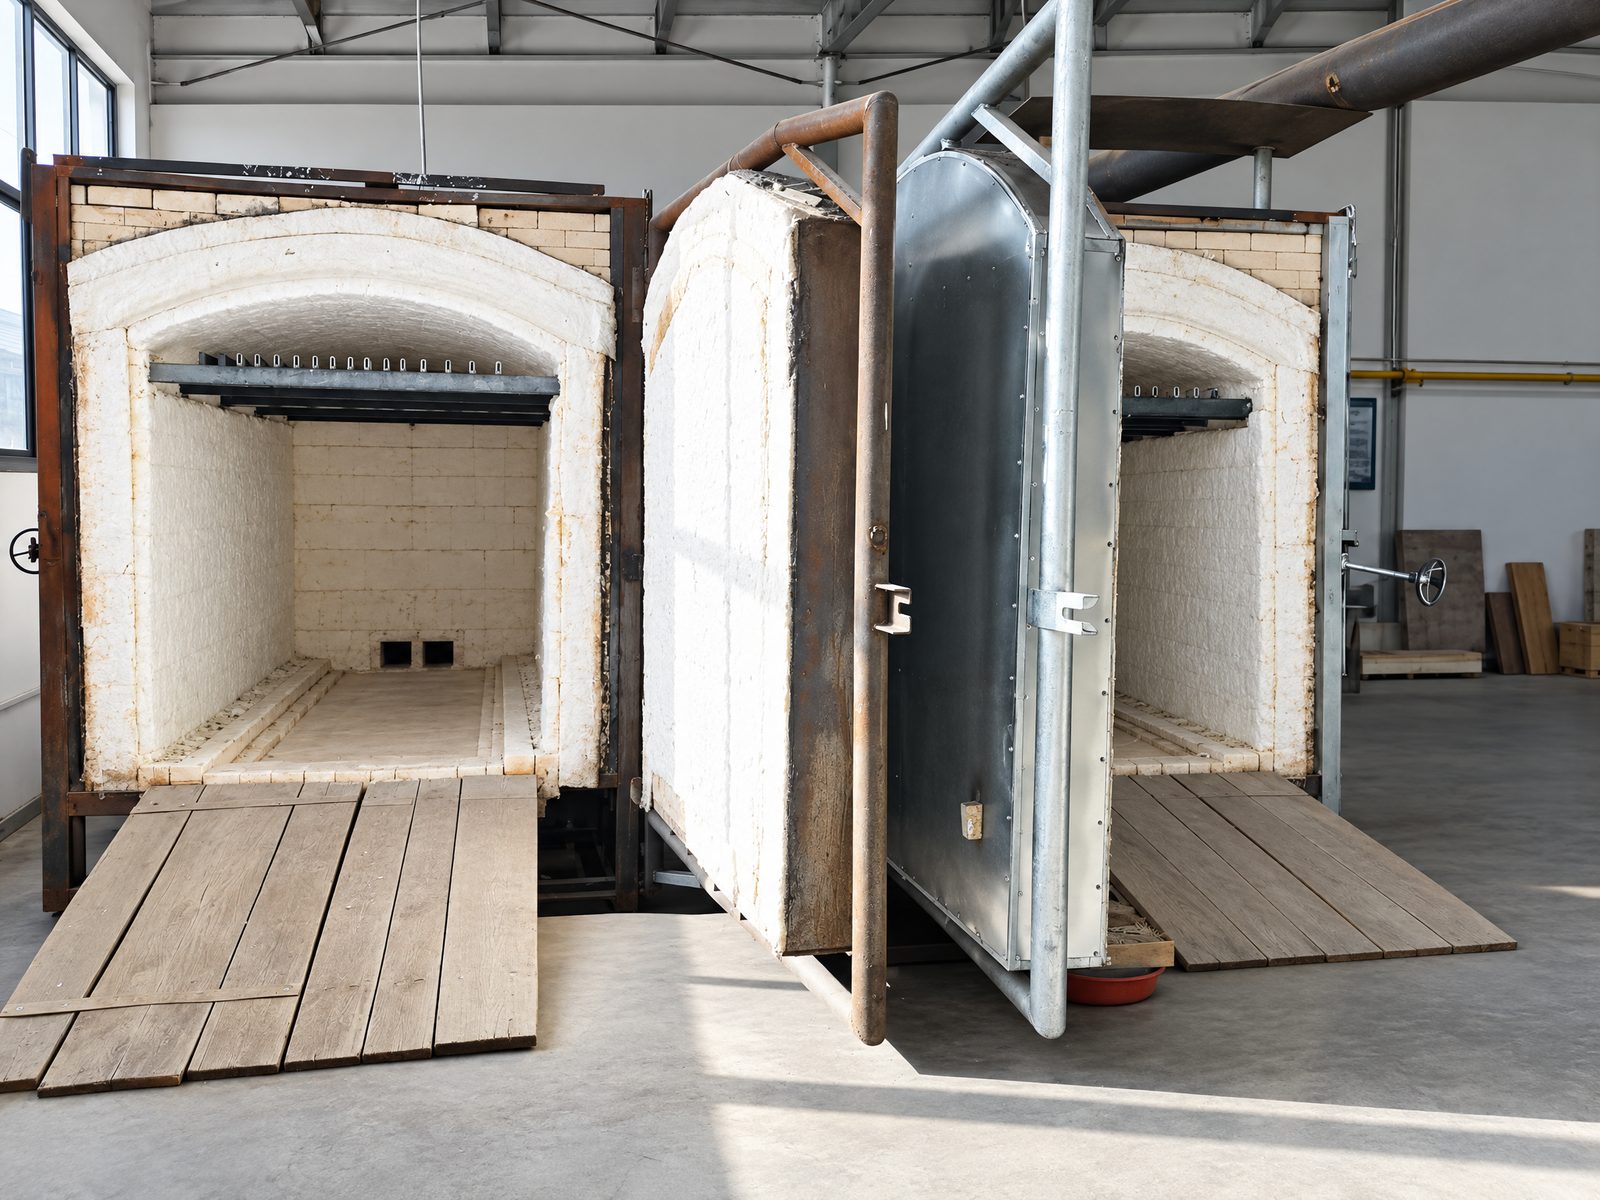
Two front-loading box kilns with arched, white fibre-lined chambers and their doors swung open.
Box kilns with fibre-lined chambers.

See the products made here

Request a quote

Send us a drawing, a sample or a part number.

Tell us the dimensions, grade and quantity. We confirm the grade, dimensions and tolerances in each quotation. Our yearly lab reports are available on request.

Custom parts, usually from
100 pcs
Samples for approval
5–10 pcs
Production, usually
25–30 days
Standard sizes from stock, small to bulk orders
~3⁠–⁠7 days